Destination
Deer Park, Texas
Deer Park severe-service procurement
Define temperature, process chemistry, corrosion mechanism, piping class and inspection before selecting the alloy component route.
Deer Park, Texas procurement context
International supply basis
RTI does not state that it has a Deer Park office, warehouse, manufacturing facility, local stock, plant contract or approval from any refinery, chemical producer or maintenance organization.
Deer Park purchasing requirements are often shaped by refinery and chemical-process conditions where pressure, temperature, process chemistry and maintenance timing cannot be separated. A nominal flange or elbow may sit in a hot hydrocarbon circuit, corrosive chemical line, steam service, utility system or outage replacement package. The RFQ should identify the line service, design conditions, piping class, material grade and UNS, applicable ASTM or ASME product standard, size, class or schedule, facing or end connection, quantity, NACE-related controls if required, examination and certificate basis.
High-alloy selection needs discipline. Inconel 625, Incoloy 825, Hastelloy C276, Alloy 20, duplex, super duplex and stainless grades solve different corrosion and temperature problems; they are not interchangeable labels. Replacement work also needs dimensional evidence because old or modified installations may not match a current standard assumption. Purchasers should identify whether examination is required before machining, after final machining or at both stages, and who has authority to release the finished dossier. RTI supports documented international supply to the agreed Deer Park destination and can coordinate PMI, dimensional reporting and TPI when specified. No local office, warehouse, inventory, refinery approval, chemical-plant contract or maintenance presence is claimed.
Flanges and pipe fittings
These genuine RTI product photographs identify the principal component families. The final quotation follows the buyer's approved material requisition, piping class and inspection scope.
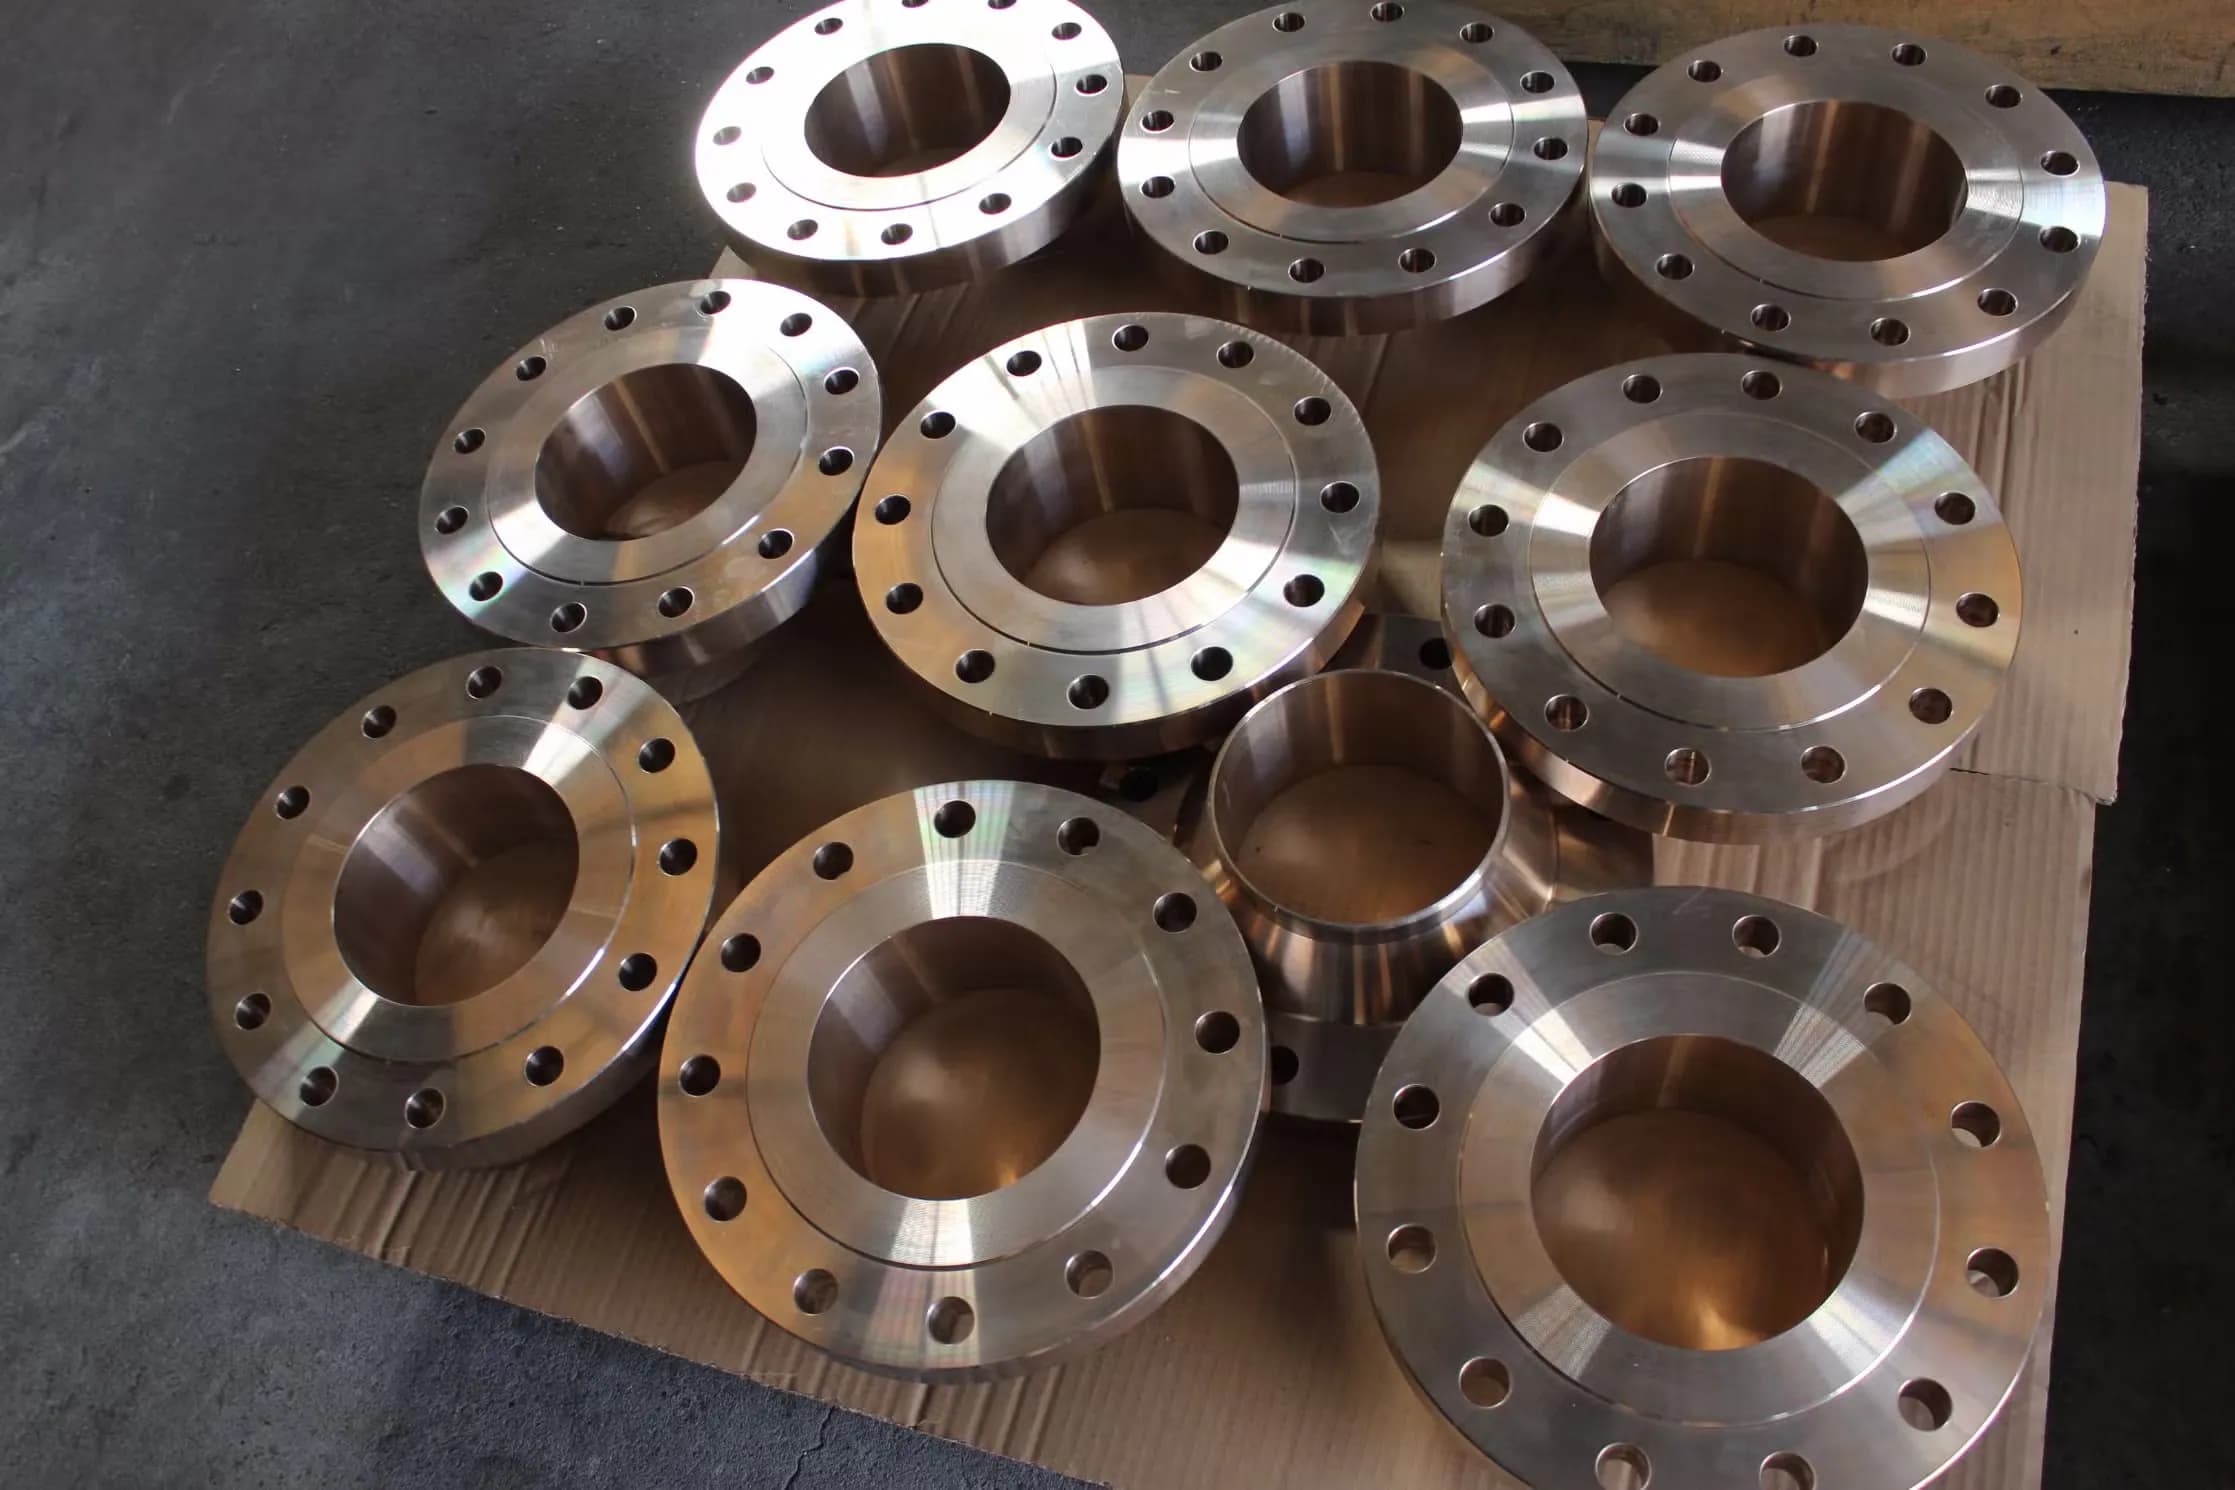
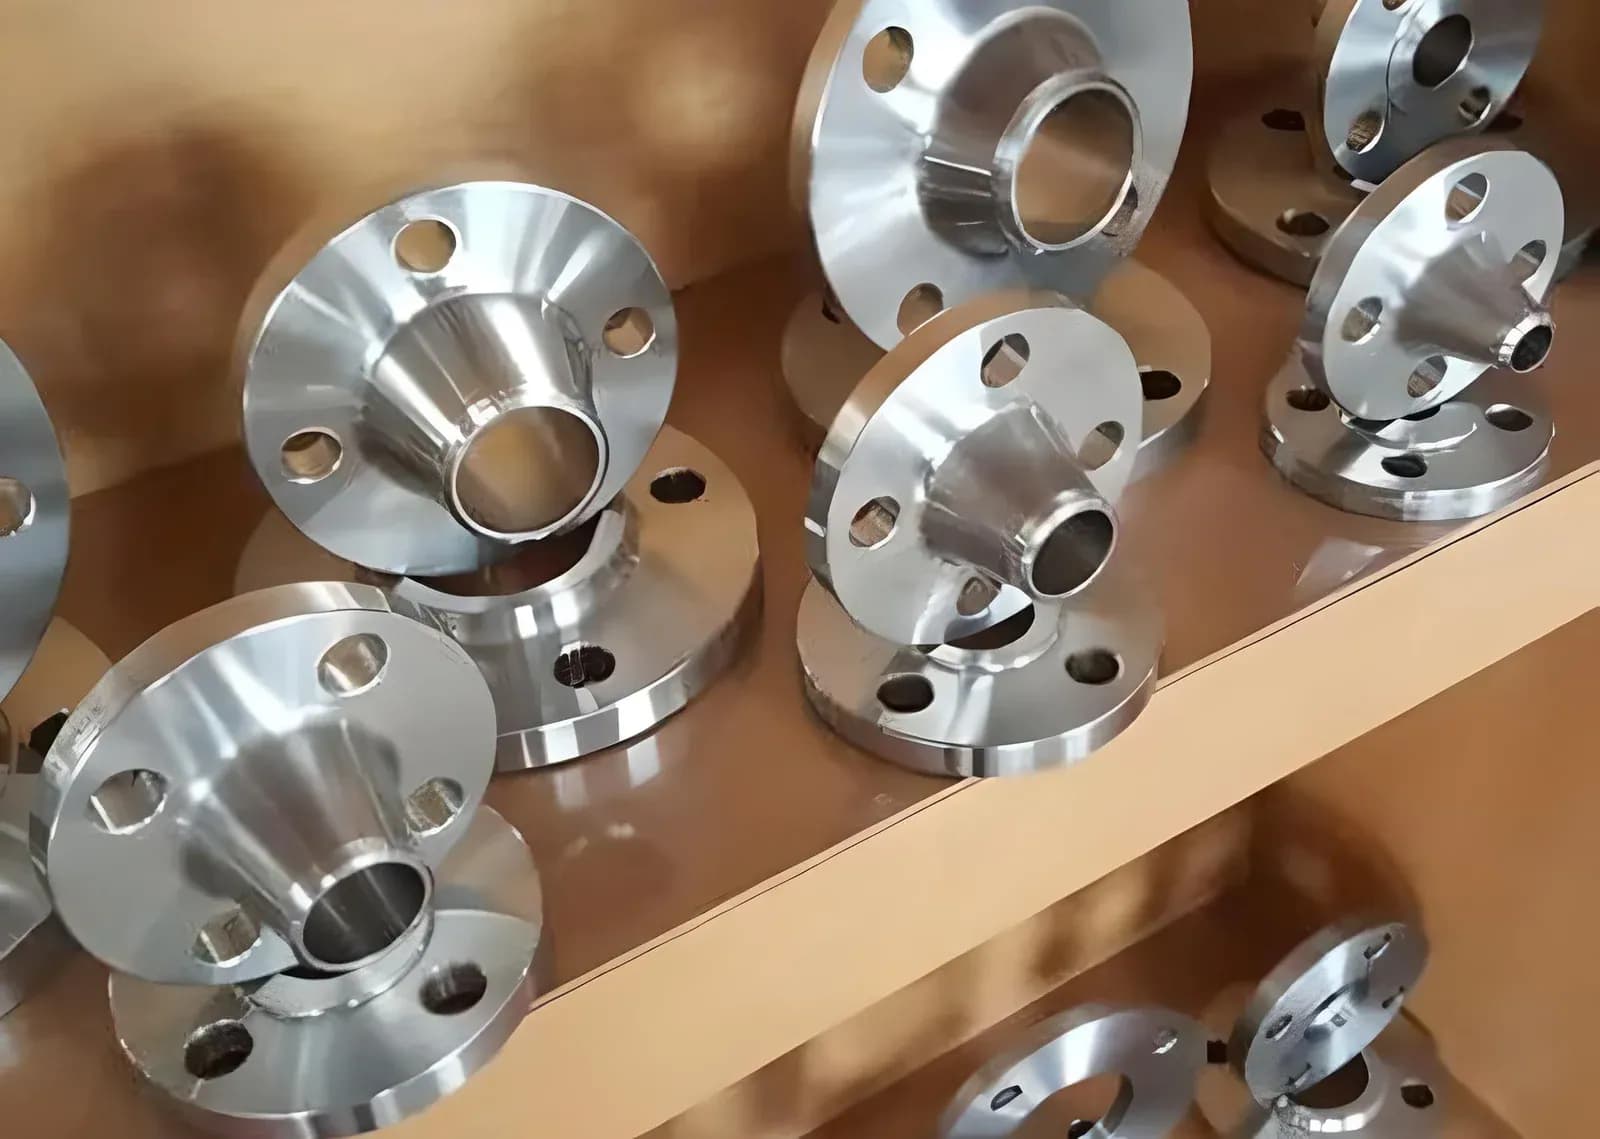
Flange enquiries may cover weld neck raised face, weld neck ring-type joint, slip-on raised face, blind, socket-weld, threaded, lap-joint, long weld neck, orifice and drawing-controlled forms. State NPS or DN, class, facing, bore or matching pipe schedule, dimensional standard and edition, quantity, material route and inspection scope.
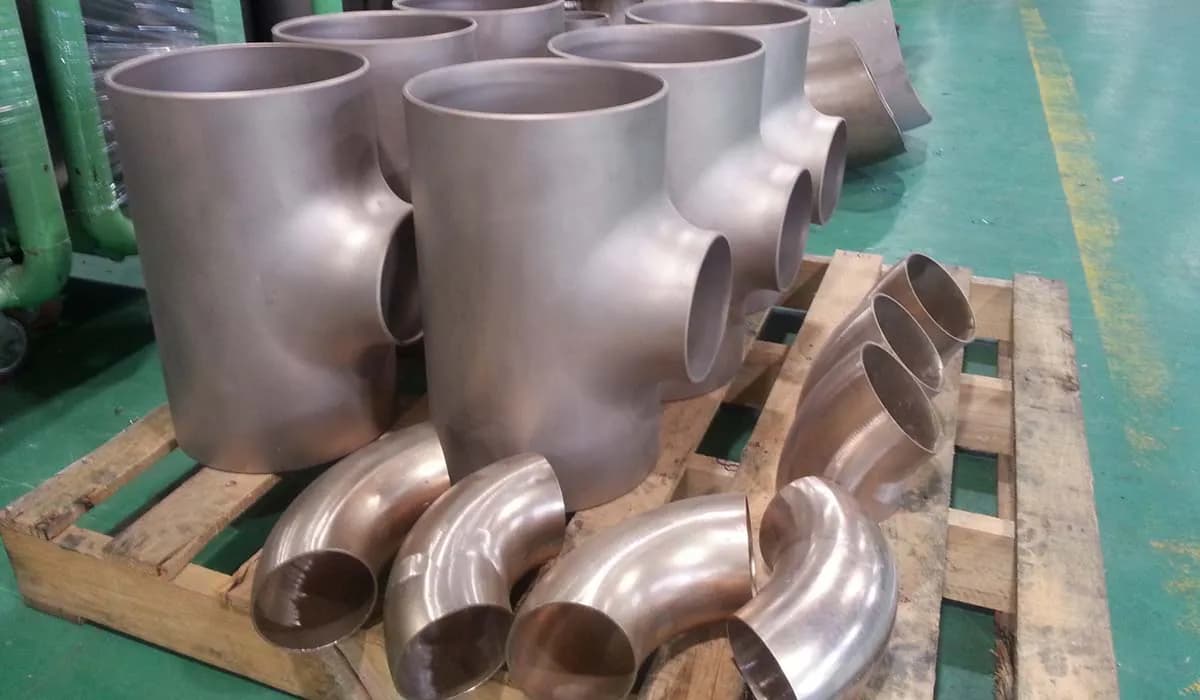
Fitting enquiries may include elbows, equal or reducing tees, concentric or eccentric reducers, caps, stub ends and crosses, plus forged socket-weld or threaded couplings, unions, nipples and branch forms. Separate wrought and forged product routes and define schedule, wall, end preparation, class, material and examination requirements.
Material priorities
The family order reflects the location's common procurement context, not a recommendation for any specific line. Project engineering must approve the exact grade and product specification.
Nickel Alloys
Consider exact corrosion chemistry, temperature, sour-service controls, fabrication route and approved product specification. Trade names are not a complete purchase description.
Review material routeStainless Steel
Match the grade to temperature, chlorides, process chemistry, cleaning regime and fabrication needs. Product-form standards differ between forged flanges and wrought fittings.
Review material routeDuplex Stainless Steel
Control the exact UNS grade, solution heat treatment, welding procedure, ferrite and corrosion-test requirements where the project specification calls for them.
Review material routeSuper Duplex Stainless Steel
Useful only when project engineering approves the grade for the chloride, seawater or severe-process duty. State the exact UNS, product standard and testing basis.
Review material routeDeer Park, Texas applications
Each application introduces different material, dimensional, inspection or delivery questions. The city context helps organize the enquiry; it never replaces the approved project specification.
Material, heat treatment, rating and code limits must be aligned to the actual design and operating envelope.
Alloy review depends on chemical species, concentration, contaminants, temperature and fabrication condition.
Hydrocarbon, sour, utility and regeneration circuits may carry different NACE, hardness and inspection controls.
Existing line data and required-on-site timing determine whether a standard or drawing-controlled route is needed.
Pressure-temperature class, corrosion allowance and material compatibility must follow the approved plant standard.
Forged socket-weld or threaded forms need exact class, bore, connection and branch-detail definition.
RTI product and inspection evidence
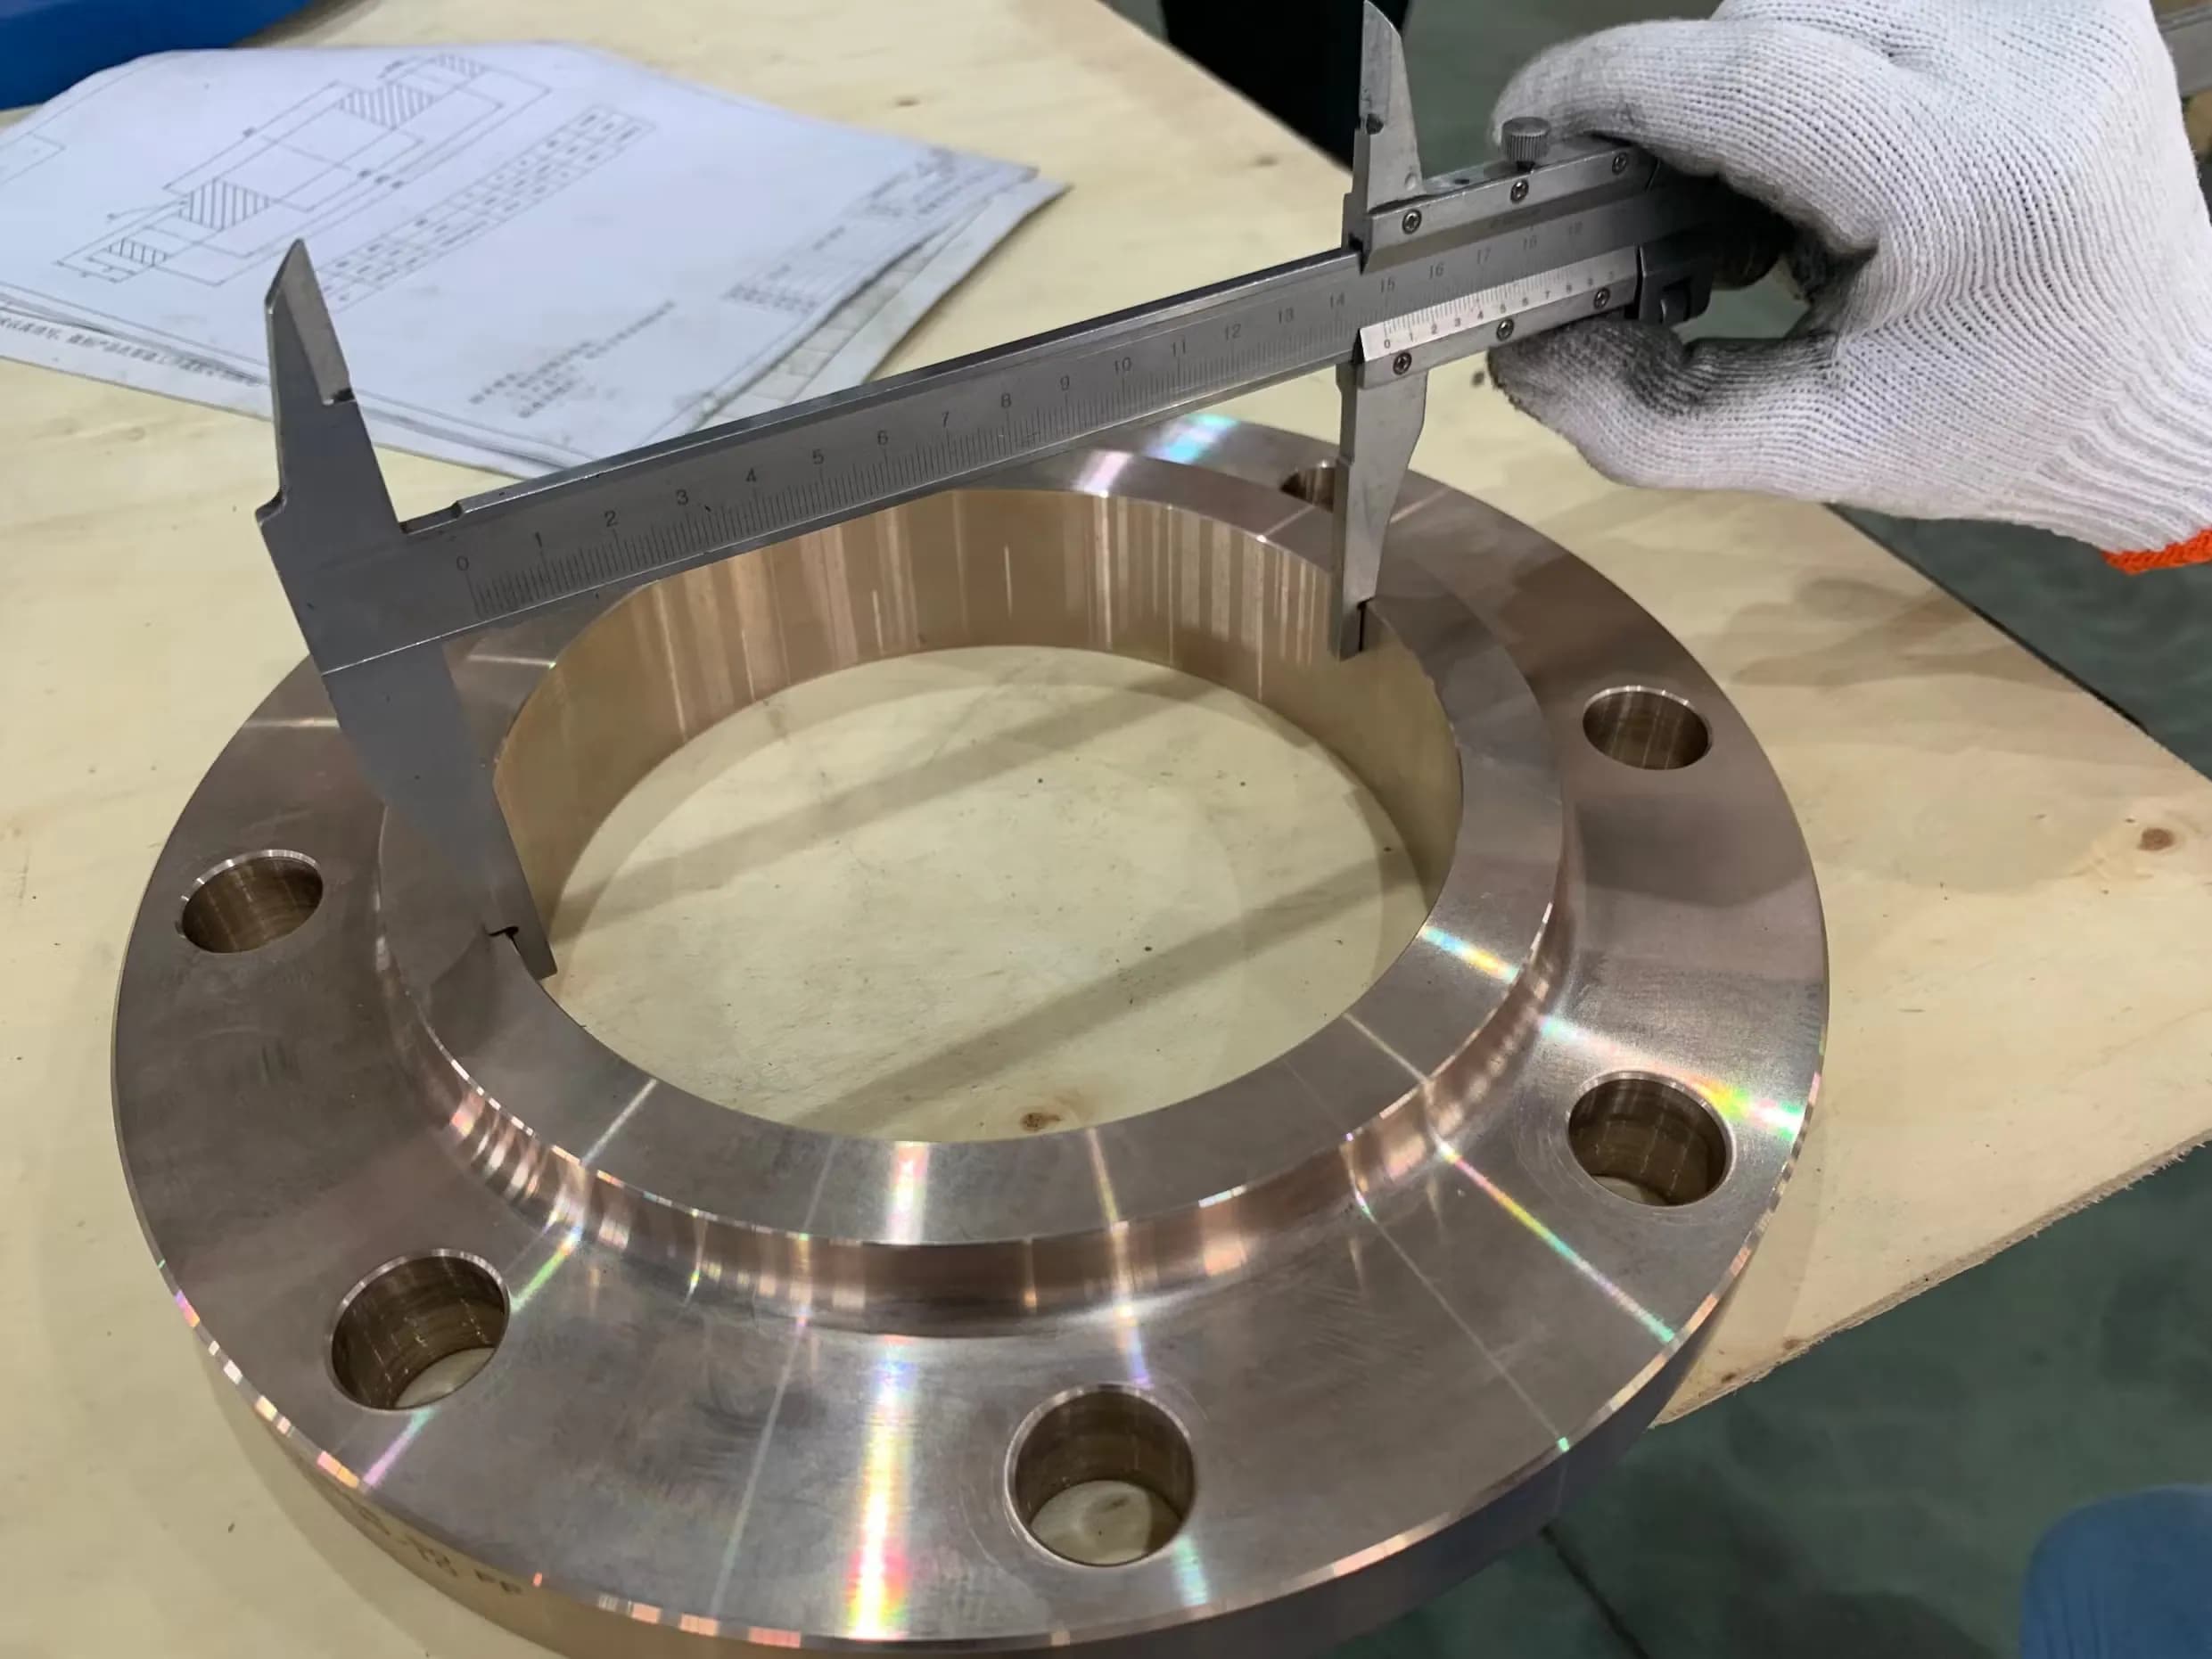
Genuine RTI photographs provide product and inspection context. They do not represent a local Texas facility, inventory position, project shipment or customer installation.
Standards and specification basis
These standards are common procurement routes, not a statement that every grade, class, size or form applies to every service. The approved project documents remain controlling.
Use the project-specified edition for applicable flange sizes, pressure classes, dimensions, bolt patterns and facings. Large-diameter requirements need their own approved dimensional basis.
Factory-made wrought butt-welding fitting dimensions must be ordered with the correct material specification, schedule or wall thickness and end-preparation requirements.
Forged socket-welding and threaded fittings require a stated class, end connection, dimensional edition and matching forged-material specification.
Orifice flange enquiries should identify the specified standard, pressure class, facing, taps, bore, assembly details and any project drawing or meter-run requirement.
Common routes include ASTM A182 for applicable forged stainless or duplex flanges, ASTM A403 or A815 for wrought fittings, and ASTM B564 or B366 for specified nickel-alloy products. Confirm the exact grade and form.
Inspection and release
Testing, inspection, documentation, marking and release requirements should be agreed before production or sourcing starts.
Define the certificate basis, heat-number transfer, component marking and document-review sequence in the purchase order. The certificate, marking and supplied grade should form one controlled traceability record.
State whether PMI is required, the sampling extent, acceptance method and report format. Alloy identity checks do not replace the full chemical, mechanical and heat-treatment requirements of the material specification.
Identify reportable dimensions, tolerances, facing finish, bore, wall thickness, bevel, bolt-hole pattern, marking and visual acceptance criteria. Drawing-based components require an approved revision.
Third-party inspection, NACE-related requirements and intergranular-corrosion testing should be specified only where the project requires them, with the agency, hold points, method and acceptance criteria agreed before release.
Related Texas routes
Use descriptive links to compare neighboring industrial contexts, then move into the relevant product, material, quality and RFQ pages.
Deer Park, Texas procurement FAQ
Deer Park, Texas technical quotation
Share material and UNS, product form, size, class or schedule, facing or connection, standard, quantity, MTC, PMI, NDE, TPI, packing, required date and the exact Deer Park, Texas delivery destination.
Technical quotation desk
Send us your material grade, size, class or schedule, quantity, and specification.